

How to Process High-Arsenic Gold Ore? An Analysis of Professional Processes and High-Efficiency Gold Extraction Solutions to Help You Easily Tackle the Challenges of High-Arsenic Gold Ore
High-arsenic gold ores are widely recognized as one of the “toughest challenges” in the field of gold ore beneficiation and smelting.Due to the high arsenic content in the ore, gold is often found in the form of fine grains encapsulated by sulfides such as arsenopyrite (FeAsS) and arsenopyrite; conventional cyanide leaching recovery rates may be as low as 30% to 60%, while reagent consumption remains high;Even more challenging is that arsenic leaches into the solution during the leaching process, creating significant environmental compliance pressures.Many mine owners are at a loss when faced with high-arsenic gold ores, sitting on resources but unable to extract the gold. This article will start with the mechanisms of arsenic occurrence to systematically analyze the processing routes, core equipment configurations, and key selection criteria for high-arsenic gold ores, providing you with a practical and efficient gold extraction solution.
I. Why Are High-Arsenic Gold Ores “Difficult to Process”? — First, Understand “Gold Displacement” and “Encapsulation”
To solve the challenges posed by high-arsenic gold ores, we must first understand why arsenic affects gold extraction. There are two core reasons:
1. Physical Encapsulation: Gold Is “Locked” Inside Arsenopyrite and Arsenic-Bearing Pyrite In
high-arsenic gold ores, gold often exists as fine particles (micrometer- or even submicrometer-sized) disseminated within the crystal lattices of arsenopyrite and arsenic-bearing pyrite, or encapsulated by them.The cyanide solution is unable to come into contact with these gold particles, resulting in naturally low leaching rates. This type of gold is referred to as “encapsulated gold” and is the fundamental reason why conventional leaching processes fail.
2. Chemical Interference: “Gold Hijacking” and Reagent Consumption
Arsenides react with cyanides in the leaching system, consuming large amounts of gold leaching reagents;some arsenic-bearing minerals also adsorb dissolved gold cyanide complexes (the “gold hijacking” effect), causing leached gold to be reincorporated into the tailings. Furthermore, the presence of arsenic in the tailings results in high treatment costs and significant environmental risks.
Conclusion: The key to processing high-arsenic gold ores does not lie in merely “tweaking the leaching conditions,” but rather in first breaking down the encapsulation and eliminating interference—this is the significance of “pretreatment.” Choosing the right pretreatment process can increase recovery rates from 50% to over 90%; choosing the wrong one means the investment goes down the drain.
II. Four Mainstream Processing Routes for High-Arsenic Gold Ore
For high-arsenic gold ores, there are four proven process routes within the industry, each with its own applicable limits. The choice of route must be based on mineral sample test data.
Route 1: Flotation Enrichment + Concentrate Pretreatment (Most Common, Most Economically Viable)
Process Logic: First, flotation is used to concentrate gold-bearing sulfides—such as arsenopyrite and arsenic-bearing pyrite—into a high-arsenic gold concentrate, significantly reducing the volume of material requiring subsequent processing (typically, the concentrate yield is only 5%–15%). The concentrate is then subjected to pretreatment and leaching.
Applicable Conditions: Gold is primarily hosted in sulfides, and the sulfides exhibit good flotability.
Advantages: Low processing volume, relatively manageable capital investment, and good economic viability; this is the most mainstream entry-level process for high-arsenic gold ores.
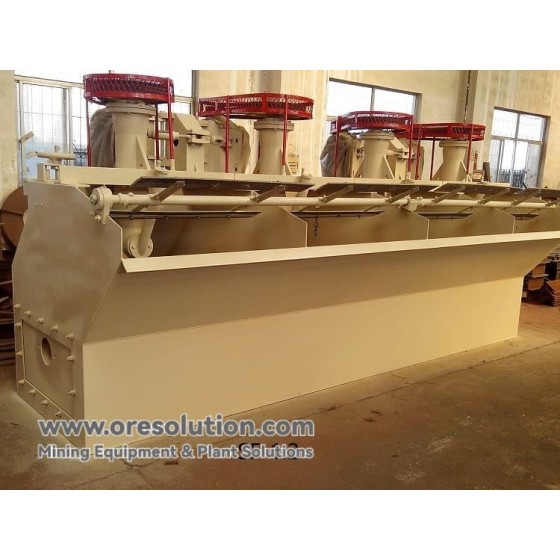
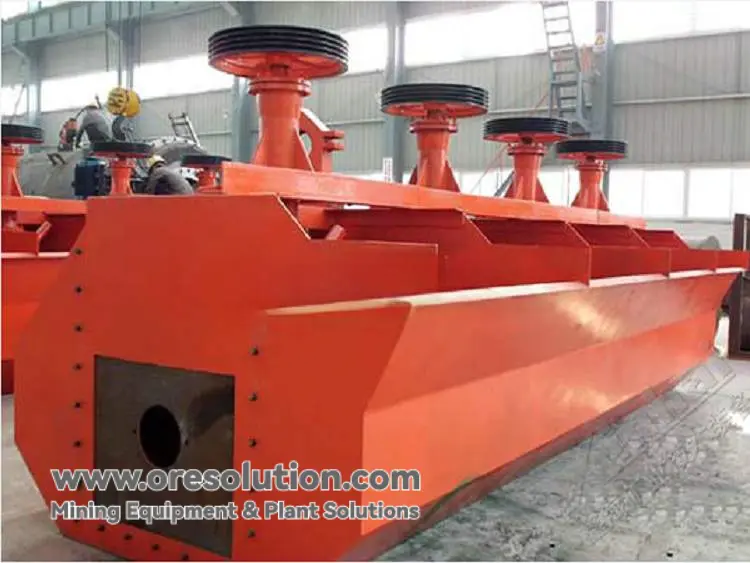
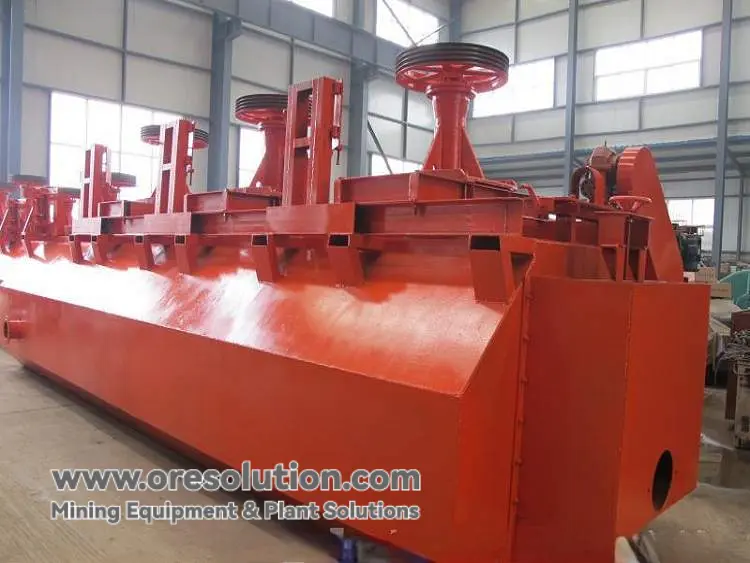
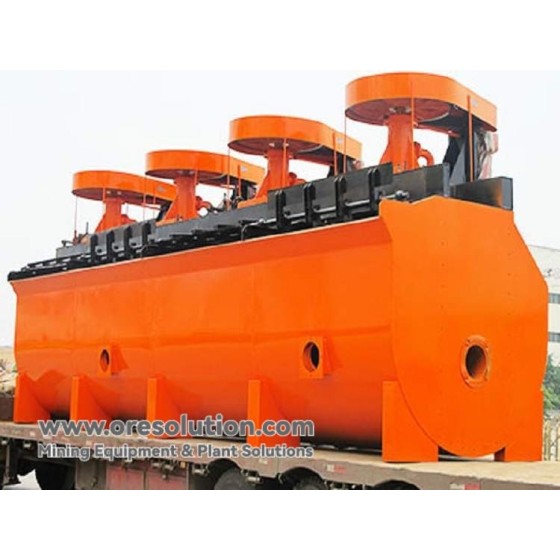
Key Equipment: Jaw crusher, cone crusher, ball mill, hydrocyclone, SF/BF-type flotation cells (roughing + scavenging + cleaning), regrinding mill, high-efficiency thickener, filter press.
Points to Note: Flotation can only “enrich” the ore, not “break up” the inclusions; the concentrate still requires pretreatment for efficient leaching; the flotation reagent regime (combination of activators, collectors, and inhibitors) must be precisely determined through testing.
Route 2: Roasting and Oxidation Pretreatment + Leaching (Classic, Well-Established Process)
Process Logic: High-arsenic gold concentrate is oxidized and roasted at high temperatures (600–800°C) in a roasting kiln, causing arsenopyrite and pyrite to oxidize and decompose. Arsenic volatilizes into the flue gas in the form of arsenic trioxide (As₂O₃), exposing the gold,followed by cyanide leaching of the roasted ore.
Suitable Conditions: Concentrates with high sulfur and arsenic content, provided the project site has the capacity to treat arsenic-containing flue gas.
Advantages: Mature technology, high adaptability, and high gold recovery rates (leaching rates for roasted ore can exceed 90%).
Disadvantages: Arsenic-containing flue gas requires a dedicated arsenic recovery system and environmental treatment facilities (quenching, electrostatic precipitators, arsenic slag solidification), entailing high environmental investment and compliance requirements; energy consumption is relatively high.
Core Equipment: Roasting kiln (rotary kiln), cooler, arsenic recovery system (quench tower, electrostatic precipitator), leaching tank, carbon-in-leach (CIL) tank, desorption and electrolysis equipment, and exhaust gas treatment system.
Points to Note: Roasting parameters (temperature, atmosphere, time) directly affect the degree of gold exposure and the arsenic volatilization rate; these must be determined through testing; arsenic slag is classified as hazardous waste and must be disposed of in compliance with local regulations.
Route 3: Bio-oxidation Pretreatment + Leaching (Environmentally Friendly Process)
Process Logic: Utilizing microorganisms such as Thiobacillus acidophilus to oxidize and decompose arsenopyrite and pyrite under acidic conditions (pH 1.5–2.0), thereby breaking down the encapsulation structure to expose the gold; the oxidized residue is then subjected to cyanide leaching.
Applicable Conditions: Suitable for projects where the concentrate or ore has moderate arsenic and sulfur content, suitable climatic conditions (temperature control required), and high environmental protection requirements.
Advantages: Environmentally friendly, no arsenic emissions in flue gas, relatively low operating costs, and suitable for small- to medium-sized projects.
Disadvantages: Long oxidation cycle (typically several days to over ten days), high requirements for temperature control and management, and the need for a stable microbial culture system.
Core Equipment: Biological oxidation tank (with aeration and agitation), aeration system, temperature control system, thickener-scrubber, leaching tank, carbon-in-leach (CIL) tank, desorption and electrolysis equipment.
Points to Note: Biological oxidation is sensitive to ore particle size, slurry concentration, and nutrient salt ratios; validation through scaled-up continuous testing is required; oxidation residue must be thoroughly washed to prevent arsenic from entering the leaching system.
Route 4: Pressurized Oxidation Pretreatment + Leaching (Highly Efficient but High Capital Investment)
Process Logic: In an autoclave, under high-temperature (180–220°C), high-pressure (1.5–3.0 MPa), and oxygen-enriched conditions, arsenopyrite and pyrite are rapidly oxidized and decomposed, and the gold is leached after exposure. The reaction is fast (typically 1–3 hours) and yields high gold recovery rates.
Suitable Conditions: Large-scale projects, mines with high arsenic and sulfur content, and mines requiring high recovery rates.
Advantages: Rapid oxidation rate, extremely high gold recovery rates (up to 95% or higher), and effective even for carbon-containing “gold-stealing” ores.
Disadvantages: High capital investment for autoclave equipment; extremely stringent material requirements (resistance to high temperature, high pressure, and corrosion); high operational and management barriers.
Core Equipment: Autoclave (made of pressure- and corrosion-resistant materials), flash cooling system, thickener-scrubber, neutralization system, leaching tank, carbon-in-leach (CIL) tank, desorption and electrolysis equipment.
Points to Note: Pressurized oxidation places extremely high demands on equipment materials and automation capabilities; it is essential to select an experienced EPC contractor. Neutralization residues must be disposed of in compliance with regulations.
Summary of Process Route Selection
| Process Routes | Applicable Scenarios | Investment | Environmental Impact | Recovery Rate |
|---|---|---|---|---|
| Flotation + Concentrate Pretreatment | Predominantly sulfide-bearing gold | Medium | Medium | High |
| Roasting and oxidation | Concentrates with high sulfur and arsenic content | Medium-high | High (arsenic flue gas) | High |
| Biological Oxidation | Small to medium-sized, with high environmental requirements | Medium | Low | Relatively high |
| Pressurized oxidation | Large-scale, high-arsenic sulfur, carbon-containing | High | Medium | Extremely high |
OreSolution\'s stance: There is no “best process,” only the “most suitable process.” The four routes can be combined (e.g., flotation enrichment followed by bio-oxidation or roasting); the final solution must be based on your ore sample\'s test report and must never simply follow a standard blueprint.
III. Core Equipment Configuration for High-Arsenic Gold Ore Processing
Taking the typical combination of “flotation enrichment + pretreatment + leaching” as an example, the core equipment for a complete gold extraction production line for high-arsenic gold ore includes:
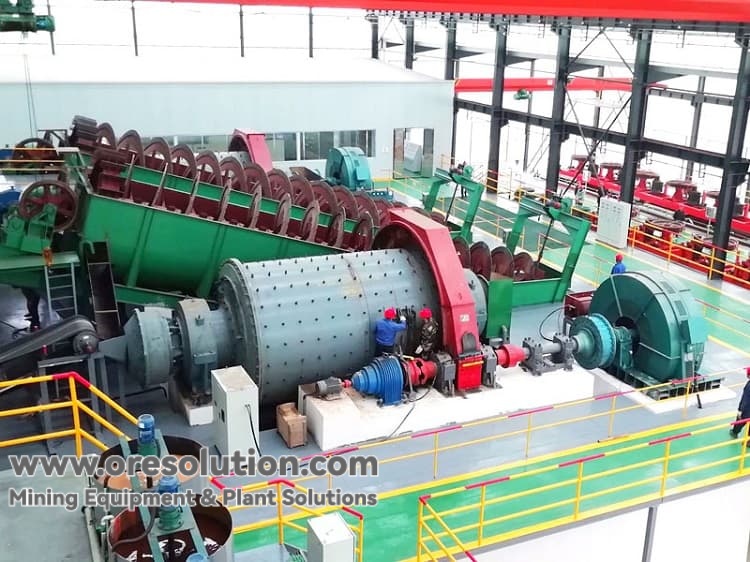
1. Crushing and Grinding Section: Jaw crusher, cone crusher, vibrating screen, ball mill, hydrocyclone, spiral classifier. The objective is to achieve single-particle liberation of gold-bearing sulfides.
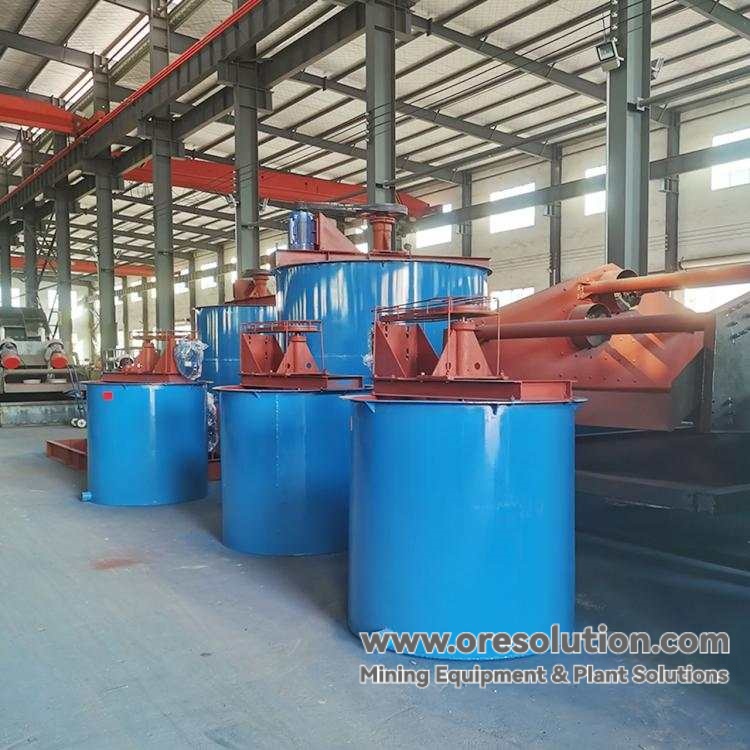
2. Flotation Enrichment Section: Agitation tanks, dosing systems, SF/BF-type flotation cells (roughing, scavenging, and cleaning), regrinding mills, high-efficiency thickeners, and filter presses. This section enriches arsenopyrite and arsenic-bearing pyrite into high-arsenic gold concentrate.
3. Pretreatment Section (selected based on the process flow):
-
Roasting: Roasting kiln, cooler, quenching tower, electrostatic precipitator, exhaust gas treatment system, arsenic slag treatment system;
-
Biological Oxidation: Biological oxidation tanks, aeration system, temperature control system, nutrient solution preparation system;
-
Pressurized Oxidation: Autoclaves, flash evaporation system, neutralization system.
4. Leaching and Recovery Section: Leaching tanks, high-efficiency dual-impeller carbon-in-leach (CIL/CIP) tanks, carbon separation screens, carbon recovery pumps, desorption-electrolysis equipment, and gold smelting furnaces. OreSolution desorption-electrolysis equipment achieves a desorption rate of over 96% and an electrolysis rate exceeding 99%.
5. Tailings and Environmental Protection Section: High-efficiency tailings thickener, filter press (dry discharge), neutralization tank, arsenic/cyanide removal treatment system, emergency storage pond. Environmental compliance is critical for high-arsenic projects; a comprehensive tailings treatment and arsenic residue disposal plan must be in place.
6. Auxiliary and Automation: Slurry pumps, water pumps, agitation tanks, electrical controls, and online monitoring (pH, chemical concentration, redox potential, etc.).
Important Note: The above represents a framework configuration; actual equipment models, quantities, and specifications must be customized based on ore characteristics, processing capacity, arsenic and sulfur content, and site conditions. Configurations may vary significantly even for the same ore type across different mining areas.
IV. Five Common Misconceptions in the Processing of High-Arsenic Gold Ore
Misconception 1: Skipping Pilot Testing and Proceeding Directly to Cyanide Leaching
If high-arsenic gold ore is leached without pretreatment, recovery rates will be low, chemical consumption will be high, and arsenic levels in the tailings will exceed standards—dooming the project to failure.Correct Approach: First, take representative ore samples to conduct mineral processing tests and comparative pretreatment tests to determine the gold occurrence state and the optimal process.
Misconception 2: Relying Solely on Flotation and Assuming Enrichment Solves Everything
. Flotation merely “concentrates” gold into the concentrate; the encapsulation structure remains intact, so the concentrate still requires pretreatment for efficient leaching. Correct Approach: A combined process of flotation, pretreatment, and leaching, with each step interlinked.
Misconception 3: Neglecting the environmentally sound disposal
of arsenic. Arsenic-containing flue gas, arsenic-containing slag, and arsenic-containing tailings are all major environmental red flags. If the roasting process lacks an arsenic recovery system and the tailings lack arsenic removal treatment, the project faces the risk of production shutdown at any time.Correct Approach: Incorporate arsenic flow paths and disposal plans into the overall design during the process design phase.
Misconception 4: Piecing Together Equipment; Mismatched
Pretreatment and Leaching Systems. Purchasing autoclaves from Manufacturer A, leaching tanks from Manufacturer B, and desorption/electrolysis units from Manufacturer C—while individual units may meet standards, system incompatibility leads to countless problems during commissioning. Correct Approach: Select an EPC supplier with in-house manufacturing capabilities for core equipment and experience in system integration.
Misconception 5: Focusing Only on Initial Investment Without Considering Operating Costs.
Cheap equipment may have a low initial investment, but it results in poor pretreatment performance, high chemical consumption, and a high failure rate; over the course of several years, the OPEX far exceeds the difference in equipment cost. Correct Approach: Calculate the return on investment (ROI) over the entire life cycle.
V. Why Choose the EPC Turnkey Model?
High-arsenic gold mine projects involve multiple stages—including pilot testing, pretreatment process design, equipment manufacturing, environmental protection facilities, and installation and commissioning—with high technical barriers and complex lines of responsibility.Under the traditional fragmented model—where “design institutes draw blueprints, equipment manufacturers sell machines, and construction crews build plant facilities”—multiple parties shift blame when performance targets are not met, forcing mine owners to act as “referees.”
Advantages of the EPC turnkey model:
-
Closed-Loop Accountability: A single team takes full responsibility for the final outcome, coordinating the entire process from pilot testing to production launch;
-
Customized Integration: Processes are tailored based on test data from mine samples, and in-house equipment manufacturing capabilities ensure seamless integration between hardware and process;
-
Proactive Environmental Compliance: The flow of arsenic, tailings treatment, and arsenic slag disposal are comprehensively planned during the design phase;
-
Cost Reduction and Efficiency Improvement: Eliminates hidden costs associated with coordinating multiple parties and shortens the plant construction timeline;
-
Reduced Design Costs: Core design phases are completed by our in-house team, saving hundreds of thousands of dollars in design fees for medium- to large-scale projects.
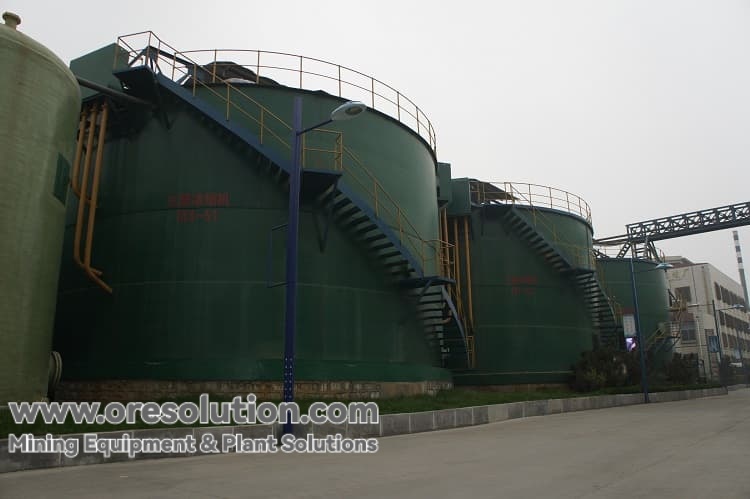
VI. OreSolution\'s Turnkey EPC Services for High-Arsenic Gold Mines
OreSolution specializes in mining equipment and mineral processing solutions, with operations spanning five major sectors: metal ores, non-metal ores, precious metal ores, alluvial deposits, and tailings/solid waste. The company operates three modern manufacturing bases (Shahe Industrial Park, Zhanggong District, Ganzhou, Jiangxi;Guzhang Industrial Park, Shicheng County, Ganzhou, Jiangxi; and Weifang Heavy Industry Park, Shandong). With 20 years of experience in mining equipment manufacturing and solution integration, our products are exported to more than 80 countries and regions worldwide. For high-arsenic gold mines, we provide comprehensive EPC turnkey services:
Step 1: Requirements Discussion and Preliminary Assessment
—We assess the ore type, gold grade, arsenic and sulfur content, associated elements, processing capacity, and site conditions to propose a preliminary process direction and feasibility assessment.
Step 2: Ore Sample Analysis and Mineral Processing Tests
: Conduct chemical composition analysis, phase analysis, and grain size determination on representative ore samples; perform flotation tests, comparative pretreatment tests (roasting/biological oxidation/pressurized oxidation), and leaching tests; and issue an authoritative “Mineral Processing Test Report,”recommend process flows, parameters, equipment selection, and expected performance indicators. This serves as the scientific foundation for the entire project.
Step 3: Customized Solution Design and Quotation
Based on the test report, we complete the Process Flow Diagram (PFD), equipment configuration list, plant site layout plan, 3D layout proposal, civil engineering requirements drawings, and environmental protection facility plans, and provide a transparent EPC (Engineering, Procurement, and Construction) budget.
Step 4: Equipment Manufacturing and Quality Inspection
Core equipment (crushers, ball mills, flotation machines, roasting kilns/biological oxidation tanks/autoclaves, leaching tanks, carbon-in-leach tanks, desorption and electrolysis equipment, thickeners, filter presses, etc.) is manufactured strictly in accordance with drawings and standards, and undergoes rigorous quality inspection prior to shipment.
Step 5: On-Site Installation Guidance and Commissioning
We dispatch senior engineers to the site to guide equipment installation, piping connections, and electrical layout; complete individual unit commissioning and full-process integrated trial runs; and conduct commissioning with water and feedstock until the production line operates stably and meets the contractually agreed-upon performance indicators.Civil engineering work is organized and carried out by the client according to the drawings; we provide technical briefings. Installation workers are sourced locally by the client, with our engineers providing on-site guidance—resulting in lower labor costs and greater flexibility.
Step 6: Personnel Training and After-Sales Support We provide systematic theoretical and hands-on training
for operators and maintenance teams (including equipment start-up and shutdown, parameter adjustment, daily inspections, and troubleshooting). We offer a 12-month warranty period, during which spare parts are replaced free of charge for quality-related issues. After the warranty period, we provide lifetime technical support at cost.
Estimated Timeline: From ore sample testing to final commissioning,the total timeline is typically 8–12 months (ore beneficiation testing: 30–45 days; engineering design: approximately 30 days; equipment manufacturing: approximately 60 days; logistics and transportation: approximately 60 days; installation and commissioning: 60–150 days). For projects involving high-arsenic, hard-to-treat ores, the timeline may be extended slightly due to the complexity of the pretreatment process.
VII. Frequently Asked Questions (FAQ)
Q: The cyanide leaching recovery rate for my high-arsenic gold ore is only 40%. Is there still a solution?
A: Yes, there is a solution, but pretreatment is required.The gold is encapsulated by arsenopyrite, preventing the cyanide solution from coming into contact with it; direct leaching will inevitably be inefficient. By using flotation enrichment combined with roasting, bio-oxidation, or pressurized oxidation to break down the encapsulation, the recovery rate can typically be increased to 85–95%. The specific process route must be determined through ore sample testing.
Q: Which is better for me: bio-oxidation or roasting?
A: It depends on the ore properties, project scale, environmental requirements, and investment budget. Bio-oxidation is environmentally friendly and has low operating costs, but the process takes a long time; roasting is a mature and efficient method, but it requires significant investment in arsenic flue gas treatment and strict compliance with environmental regulations. We recommend conducting ore sample tests first to compare the recovery rates and economic viability of both routes.
Q: How are arsenic slag and arsenic-containing tailings treated?
A: Arsenic slag must be disposed of in compliance with hazardous waste regulations or local laws (safely stockpiled after solidification/stabilization), while arsenic-containing tailings must be neutralized and treated to remove arsenic until they meet regulatory standards before being recycled or discharged. The flow of arsenic and disposal plans must be comprehensively planned during the process design phase; this is a key component of the EPC contract.
Q: What recovery rate can you guarantee?
A: The recovery rate depends on the characteristics of the ore itself (gold occurrence, arsenic and sulfur content, grain size of gold particles, etc.).We do not make unfounded promises; rather, we commit to the following: through rigorous mineral processing tests, we will design a process that achieves the highest possible recovery rate under the specific conditions of the ore, and we will strive for excellence in equipment selection and process control to ensure that actual production performance closely matches the test results.
Q: My mine is overseas. Can you provide on-site support?
A: Yes. We export equipment to over 80 countries and offer technical coordination in English or bilingual formats. Our expert engineers can travel to the site to guide installation, conduct commissioning with actual ore, and provide staff training. We are familiar with logistics routes in Africa, Southeast Asia, South America, Central Asia, and the Middle East.
Q: Are there fees for testing and design?
A: We charge a basic service fee, which is reasonable. Upon signing an equipment or EPC contract, the initial testing and design fees can be fully offset against the equipment cost. Testing services can also be purchased separately; there is no obligation to enter into subsequent cooperation.
VIII. High Arsenic Content Is Not a Dead End—Choosing the Right Process Is Key
High-arsenic gold ore processing is challenging because the gold is encapsulated, arsenic interferes with the process, and environmental regulations impose strict requirements.However, there are proven technical approaches within the industry to address these challenges—flotation enrichment, roasting and oxidation, bio-oxidation, and pressurized oxidation. Each of these four approaches has its own applicable scope; the key is to select the right approach based on your ore sample test data and to implement the process through a closed-loop EPC responsibility system.
OreSolution\'s approach is clear: testing first, design second. A single team takes full responsibility for the final outcome, providing end-to-end EPC turnkey delivery—from ore sample testing, process design, equipment manufacturing, installation, and commissioning to personnel training.Conventional processes ensure minimum performance, while proprietary technologies maximize potential—whether your high-arsenic gold ore consists of arsenopyrite, arsenic-bearing pyrite with gold, or carbon-bearing “gold-bearing ore,” we have specialized solutions tailored to your specific needs.